 EN
Contact Us
Building 4, Power Valley Industrial Park, Majiahe Street, Tianyuan District, Zhuzhou City, Hunan Province, China
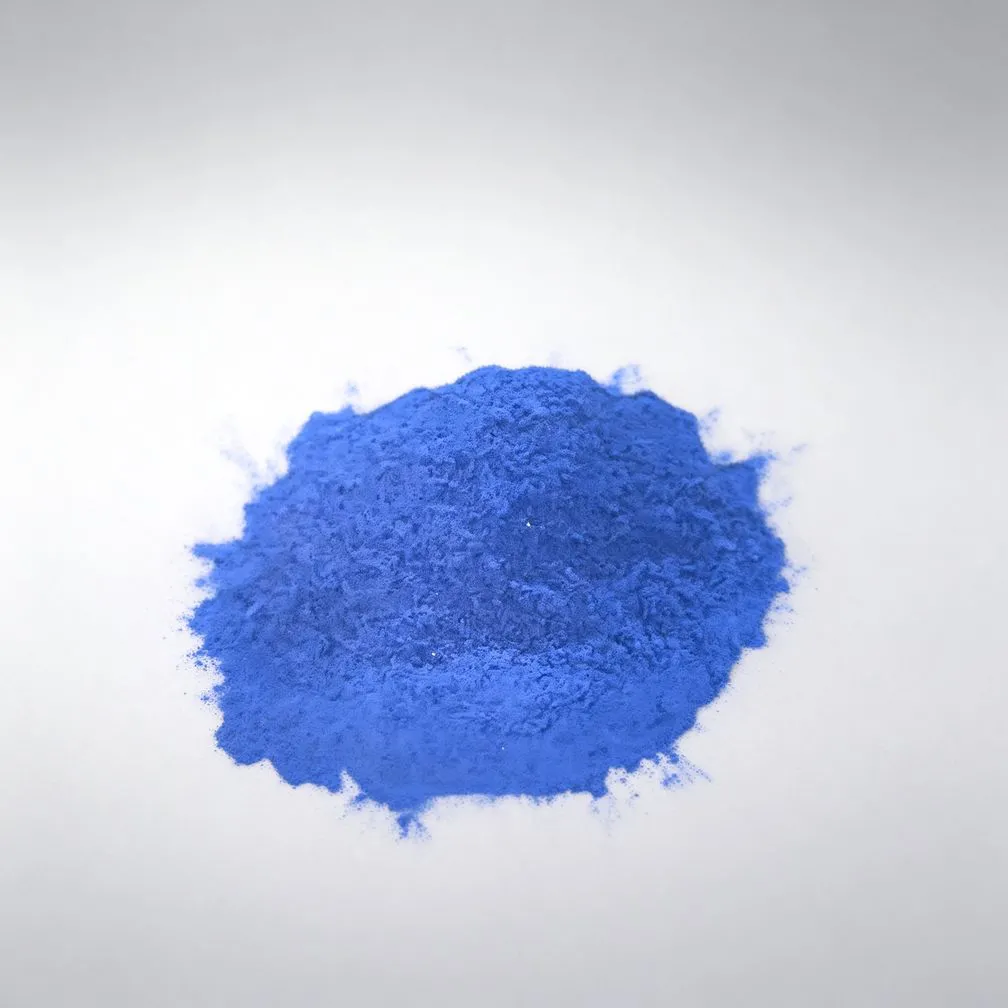
Blue Electrostatic Enamel Powder for Water Heater Tanks
A blue powder for dry electrostatic enameling of water-heater tanks, with an acid-resistance result recorded on the citric acid test.
Product Description
Blue porcelain enamel powder for dry electrostatic application on steel, fired at a nominal 850 °C, for water-heater tanks. A glossy blue finish with an acid-resistance result recorded on the citric acid test.
- FinishBlue glossy
- Firing850 °C nominal
- Acid resistanceA+
- AdhesionGrade 1–2
What the material does well
- No slurry preparation or drying step. The powder is applied dry, and the coated part goes from the booth to the furnace.
- A single firing after coating. The finish is formed in one firing; no separate drying stage sits between spraying and firing.
- Film build controlled during spraying. The deposited layer depends on the equipment settings, part geometry and line conditions.
Technical data
Product specifications
| Parameter | Specification |
|---|---|
| Substrate | Low-carbon cold-rolled steel; enamel-grade steel recommended |
| Surface preparation | Degreasing or acid pickling as the part requires; no rust, dust or oil before coating |
| Application method | Dry electrostatic spraying |
| Firing temperature | 850 °C (reference value, on steel; not a fixed setting for every part) |
| Colour | Blue |
| Surface finish | Glossy |
| Adhesion | Grade 1–2 |
| Acid resistance | A+ on the citric acid test |
A+ is a result recorded on the citric acid test, not a certified or general rating.
What the line has to provide
- Substrate and pre-treatment. Low-carbon cold-rolled steel, prepared as set out under Technical data before the part reaches the booth.
- Electrostatic equipment. A high-voltage generator and a spray gun able to reach the surfaces that have to be coated.
- Furnace capability. A furnace able to reach the nominal 850 °C with the load in it.
- Firing conditions assessed on the part. The setting and dwell that suit a given part follow its size, mass and geometry and the way the furnace is loaded, and are agreed with our technical team.
Outside this range: this grade is confirmed for low-carbon cold-rolled steel. Cast iron, stainless steel, aluminum, galvanized steel and pre-coated steel are outside the confirmed scope of this grade; a part in one of those substrates is assessed separately with our technical team, and other product ranges are specified separately.
Questions we are asked
- Is a drying step needed after spraying?
- No. The part goes from the booth to the furnace; there is no intermediate drying stage.
- Is the dry process suitable for a tank?
- It depends on the surfaces that have to be coated and on the booth and handling equipment at your plant. Send the tank drawing and we will assess the route.
- What do you need to assess an application?
- The substrate grade and thickness, the part and its geometry, the application method available at your plant, and the firing equipment you can reach.
Next step
Send the tank drawing, the substrate and your firing conditions. We will confirm whether the dry process fits the part and take the firing assessment from there.
Send the part detailsValues describe the grades, not a guarantee for a particular part. The data sheet issued with a quotation carries the binding figures.